At Media Center
You Can Access Our Press Releases
(October 19, 2026, Washington, D.C., USA) On the evening of October 18th local time, the 2026 International Society for Pharmaceutical Engineering (ISPE) Facility of the Year (FOYA) Awards Ceremony was held in Washington, D.C., USA. Representatives from global pharmaceutical companies, engineering institutions, and the life sciences field gathered to witness the annual innovative achievements in the pharmaceutical engineering field. As a winner in the 2026 FOYA "Innovation – Novel Technology" category, Hepalink Pharmaceutical Group Co., Ltd.’s Shenzhen Hepalink Pingshan New Pre-filled Syringe Manufacturing Facility (the “Pingshan facility”) was recognized alongside projects from leading global pharmaceutical companies such as Sanofi, Bayer, and Eli Lilly, and is the only Chinese pharmaceutical company project among the eight category winners this year. A delegation from Hepalink Pharmaceutical attended the awards ceremony and accepted the award on stage.
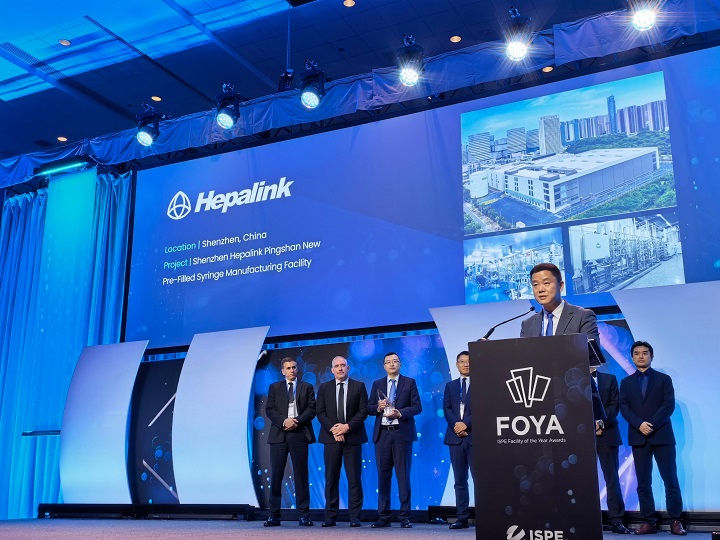
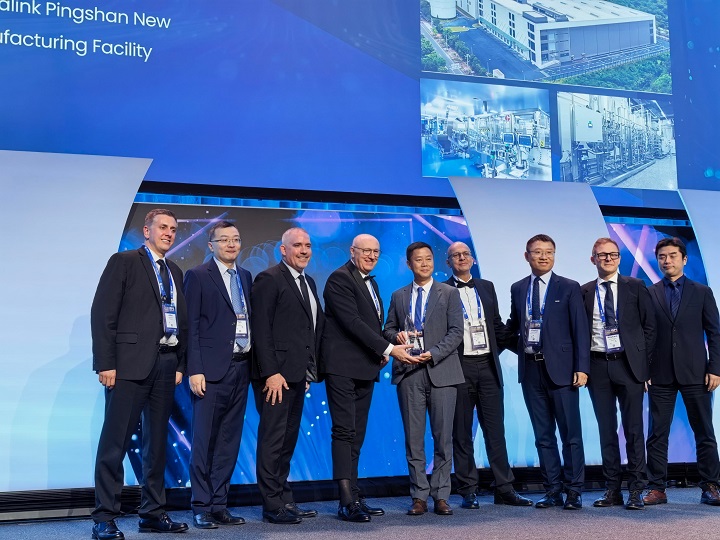
▲Scene from the 2026 ISPE FOYA Awards Ceremony
From a future-oriented formulation manufacturing facility in Shenzhen, China, to the world stage of pharmaceutical engineering, Hepalink Pingshan New Pre-filled Syringe Manufacturing Facility showcases a new practice of Chinese biopharmaceutical companies participating in global industrial exchanges with advanced manufacturing capabilities.
At the ceremony, Francesco Intoccia, a senior judge at FOYA and senior vice president of global engineering, environmental health safety and sustainability at GlaxoSmithKline (GSK) , mentioned the significance of the Hepalink intelligent manufacturing project for the global supply of critical anticoagulant drugs. "The project integrates advanced digital technology, AI-driven processes and 'zero-touch' logistics, and improves product quality, production efficiency, supply resilience and patient safety through an integrated production system."
For Hepalink Pharmaceuticals, the development of advanced manufacturing capabilities has always served the purpose of ensuring drug quality and global supply stability. For a long time, Hepalink has continuously provided stable and reliable products and services to the global market through its comprehensive quality, production, and supply chain systems; and from its inception, this project's innovations and new technologies have been dedicated to ensuring the safety and stability of global drug supply.
"This is not only an acknowledgment of a facility, but also an acknowledgment of the innovative concepts, technological exploration, and teamwork behind it," said the representative of Hepalink Pharmaceuticals in his acceptance speech.
The Pingshan facility can achieve an annual production capacity of 330 million pre-filled syringes, and its system design revolves around intelligent manufacturing, high-quality assurance, and global supply collaboration. In terms of intelligent manufacturing, the project adopts a 24-meter-high automated three-dimensional warehousing system to optimize material storage and transfer processes; it also introduces AI visual inspection technology to improve defect identification capabilities during high-speed production. Regarding quality assurance, the project combines isolator filling and automated logistics solutions to enhance the ability to maintain a sterile production environment.
At the same time, the project integrates production, quality, and operational data to achieve information synergy in key areas and further explores cross-park collaboration models. By connecting the digital systems of Pingshan and Nanshan parks, it enables the linkage of production planning, inventory management, quality information, and operational data, thereby improving the collaborative efficiency and operational capabilities of the group's global manufacturing network.
The global pharmaceutical industry is undergoing continuous changes in its manufacturing models. With increasingly stringent regulatory requirements , evolving supply chain environments, and increasingly diversified market demands, pharmaceutical companies need to continuously improve the adaptability of their facilities and operating systems. Hepalink's intelligent manufacturing project represents an exploration of the future of pharmaceutical manufacturing within this context.
Having cultivated the heparin field for nearly 30 years, Hepalink Pharmaceuticals has continuously participated in global pharmaceutical supply chain collaboration. From the entry of heparin raw materials into the international market, to the approval of enoxaparin sodium formulations in 81 countries and regions worldwide and their commercialization in more than 50 countries and regions, and further to the construction of an advanced manufacturing system that meets international quality standards, Hepalink Pharmaceuticals has continuously deepened its platform-based capabilities covering products, quality, manufacturing, and global operations.
In the field of life and health, scientific standards, quality requirements, and patient value have always been core concerns shared by the global pharmaceutical industry. Hepalink Pharmaceuticals consistently adheres to international regulations and quality system requirements in its global operations, continuously investing in manufacturing capabilities and compliance systems to work with partners from different countries and regions to promote safe and accessible medicines.
In the future, Hepalink will continue to explore the connection between advanced manufacturing and life and health needs, and work with more global partners to bring trustworthy medicines and services to more patients through more mature products, quality and operation systems.
About ISPE FOYA
The ISPE Facility of the Year Awards (FOYA) recognizes outstanding projects that set benchmarks in the global pharmaceutical and biopharmaceutical manufacturing industry. The 2026 winners span multiple continents and therapeutic areas, showcasing the continued progress of global pharmaceutical manufacturing in areas such as innovation, operational efficiency, supply chain collaboration, Pharma 4.0™, and social impact.
This year's award-winning projects showcase multidimensional upgrades in the design, construction, and operation of pharmaceutical facilities, encompassing modular and digital manufacturing pathways, sustainable infrastructure development, more efficient project execution, and integrated collaboration in quality and supply systems. Overall, these projects demonstrate the crucial value of engineering, advanced manufacturing capabilities, and cross-functional collaboration in addressing evolving regulatory requirements, operational challenges, and societal needs. They also reflect the ongoing evolution of the global pharmaceutical manufacturing system towards higher quality, greater reliability, and a more patient-centric approach.
Official WeChat Account